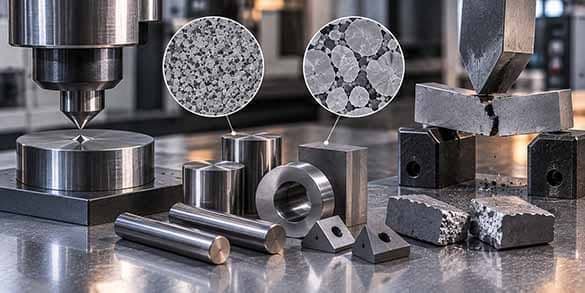
Hardness vs. Toughness in Tungsten Carbide: Understanding the Engineering Tradeoff
Learn how hardness, toughness, WC grain characteristics, binder system, geometry, and loading conditions interact to influence cemented tungsten carbide performance.
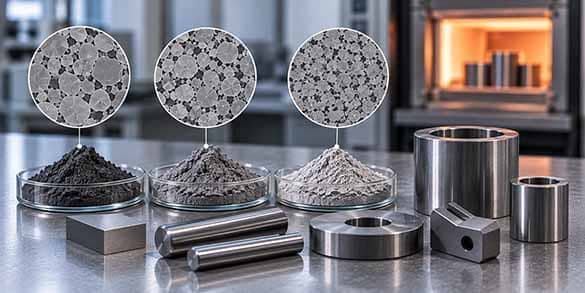
The performance of cemented tungsten carbide is closely linked to its microstructure. Understanding how WC grain characteristics, binder type and content, density, porosity, sintering quality, and manufacturing consistency influence material behavior helps engineers make better material-selection decisions for severe-service applications.
Rather than treating tungsten carbide as a single material with fixed properties, it is more useful to view cemented tungsten carbide as an engineered composite material. Its hardness, toughness, wear resistance, corrosion behavior, and dimensional performance depend on grade design, manufacturing control, component geometry, and actual operating conditions.
Cemented tungsten carbide typically consists of:
The WC phase provides high hardness and resistance to abrasive and erosive material loss, while the metallic binder holds the WC grains together and contributes toughness and structural cohesion.
The performance of a carbide grade therefore depends on the balance between the hard phase and the binder phase—not on hardness alone.
Cemented tungsten carbide is a composite material consisting of tungsten carbide grains bonded together by a metallic binder phase.
It can be engineered to provide a combination of:
Compared with many conventional metallic materials, cemented tungsten carbide can provide significantly greater resistance to abrasive wear, particle erosion, and progressive dimensional loss.
However, its performance depends on the selected carbide grade, component geometry, support conditions, manufacturing quality, and actual service environment.
The performance of cemented tungsten carbide is influenced by several interconnected variables, including:
Finer WC structures generally support higher hardness and can provide strong resistance to micro-cutting and certain forms of abrasive or erosive wear.
Carbide structures designed for greater toughness may be more suitable where impact, bending, vibration, stress concentration, or other mechanical loads increase the risk of cracking, chipping, or edge damage.
There is no universally optimal WC grain structure or binder content. The appropriate balance depends on the dominant wear mechanism, mechanical loading, component geometry, environment, and required failure resistance.
Carbide performance depends not only on nominal grade composition but also on how consistently the intended microstructure is produced.
Important manufacturing factors include:
Variations in these factors can influence hardness, toughness, dimensional accuracy, defect population, surface integrity, and ultimately component performance.
For severe-service applications, consistent manufacturing and quality control are therefore essential parts of carbide material engineering.
The properties of cemented tungsten carbide are interconnected. Changing one characteristic can affect others, which is why carbide grades should be selected according to the actual application rather than a single maximum property value.
Important engineering characteristics include:
The optimum carbide grade is therefore not necessarily the hardest or toughest grade. It is the material whose combination of properties best matches the dominant wear mechanisms, mechanical loads, chemical environment, component design, and required service performance.
Different wear mechanisms interact with the WC grains and binder phase in different ways. In many severe-service applications, more than one mechanism acts at the same time.
Hard particles or contacting surfaces can progressively remove material through scratching, micro-cutting, plowing, binder-phase damage, grain-scale fracture, or loss of support around WC grains.
The resulting wear behavior depends on particle hardness, size and shape, carbide microstructure, binder system, contact pressure, sliding conditions, and component geometry.
Particles carried by a moving gas or liquid can repeatedly strike the carbide surface.
Depending on particle velocity, size, shape, concentration, impact angle, and material properties, damage may involve:
The most suitable carbide microstructure can vary with the erosion conditions. A grade that performs well under low-angle cutting may not provide the same performance under high-angle particle impact.
Impact, bending, vibration, cyclic loading, and local stress concentration can initiate cracks or edge damage when stresses exceed the capability of the carbide grade and component design.
For these applications, toughness, wall thickness, edge geometry, support, load distribution, mounting method, and carbide-to-metal interfaces can be as important as hardness.
Slurry environments can expose carbide components to a combination of abrasive particles, fluid-driven erosion, repeated particle impact, and chemical attack.
Performance depends on factors such as particle concentration, particle hardness, velocity, impact angle, fluid chemistry, temperature, and the interaction between the WC grains and binder phase.
Because several damage mechanisms may operate simultaneously, slurry-wear resistance should be evaluated under conditions that represent the actual application as closely as practical.
In chemically aggressive environments, corrosion of the binder phase can reduce support around WC grains. Mechanical wear may then remove the weakened material, exposing fresh surfaces to further chemical attack.
This interaction can produce material loss that is more severe than would be expected from corrosion or mechanical wear considered independently.
Cemented tungsten carbide can retain high hardness and wear resistance under demanding operating conditions, but temperature and chemical exposure must be evaluated on an application-specific basis.
Performance can be influenced by:
In certain corrosive environments, the binder phase can experience preferential chemical attack. Alternative binder systems, including nickel-based grades, may therefore be considered when corrosion resistance is an important design requirement.
However, binder selection should be based on the specific chemical environment and required mechanical properties. A change intended to improve corrosion resistance can also affect hardness, toughness, manufacturing behavior, and overall wear performance.
For elevated-temperature service, material selection should account for the carbide grade, binder system, component geometry, thermal expansion differences, thermal gradients, interfaces, and surrounding assembly.
Cemented tungsten carbide is available in many engineered grade combinations because different applications require different balances of material properties.
Grade design can vary through:
As a result, carbide grades can be engineered toward different priorities, such as:
Grade selection should therefore begin with the actual failure mechanism and operating conditions rather than with a generic grade designation or the highest available hardness value.
Selecting cemented tungsten carbide is not simply a matter of choosing the hardest available grade.
Reliable severe-service performance depends on matching:
Understanding these relationships allows engineers to select, validate, and refine carbide grades more effectively for high-wear industrial components.
For custom tungsten carbide components, material selection should be reviewed together with drawings, tolerances, surface requirements, mating materials, loading conditions, wear mechanisms, and the expected operating environment.
Understanding carbide microstructure, WC grain characteristics, binder systems, sintering quality, hardness and toughness helps engineers make better material decisions for severe-service components.
There is no universal optimum WC grain size. The most suitable microstructure is the one that matches the application’s wear mechanisms, mechanical loading, environment, and component design.
The performance of cemented tungsten carbide is closely linked to its microstructure.
Two carbide materials can contain similar proportions of tungsten carbide and metallic binder yet behave differently in service because their microstructural characteristics differ, including:
For this reason, carbide grade selection should not be based on binder content or hardness alone.
WC grain characteristics influence the balance between hardness, toughness, abrasive-wear resistance, erosion resistance, crack behavior, and resistance to dimensional wear. However, grain size should never be considered independently of the binder system, manufacturing quality, component geometry, and actual service conditions.
This article explains how WC grain characteristics and microstructure influence cemented tungsten carbide performance—and why there is no single “best” grain size for every application.
Cemented tungsten carbide is a composite material consisting primarily of:
The WC phase provides:
The metallic binder contributes:
The final performance of the material is therefore not determined by either phase alone. It results from the interaction between WC grain characteristics, binder system, microstructural quality, and manufacturing control.
“Grain size” is often used as a convenient description of carbide microstructure, but average grain size alone does not fully characterize the material.
Relevant WC characteristics can include:
These variables influence how the material responds to:
A carbide specification based only on nominal binder percentage may therefore be incomplete if the application is sensitive to microstructural behavior.
Finer WC structures generally support higher hardness.
This can be advantageous in applications where the dominant damage mechanism involves:
A finer structure can reduce the scale of individual WC features interacting with abrasive particles and may improve resistance to certain forms of abrasive or erosive wear.
However, finer is not automatically better. The performance of a fine-grained carbide still depends on:
Where mechanical shock, bending, edge loading, vibration, or other fracture-related conditions become important, maximum hardness may not provide the best overall performance.
Coarser WC structures are often associated with a different hardness–toughness balance than finer structures.
Depending on binder content and the complete microstructure, such structures may be considered where the application requires greater tolerance of:
However, “coarser grains equal tougher carbide” should not be treated as a universal rule.
Toughness depends on the complete material system, including:
A coarser material may also provide lower hardness or abrasive-wear resistance than required for another application.
The engineering objective is therefore not to maximize or minimize grain size. It is to establish the microstructure that provides the required balance of properties.
Average grain size is only one part of microstructural control. The distribution of WC grain sizes can also influence material behavior.
An inconsistent microstructure may contain:
These features can create local differences in:
For severe-service components, repeatable performance therefore depends not only on achieving a target nominal grade but also on maintaining a consistent microstructure from part to part and batch to batch.
During sintering, some WC grains may grow more rapidly than the surrounding microstructure.
If excessive, abnormal grain growth can reduce microstructural uniformity and create local regions that behave differently from the intended grade structure.
The significance of abnormal grains depends on:
Controlling abnormal grain growth can involve:
The objective is not necessarily to create the narrowest theoretically possible grain-size distribution. It is to produce the intended, stable, and repeatable microstructure for the selected grade.
Certain additives may be used in carbide formulations to influence WC grain growth during sintering.
Depending on the grade design, these may include:
The role and concentration of these additions are specific to the grade design, manufacturing process, and intended application. They should not be treated as universal requirements for high-performance carbide.
An addition that is useful for one microstructural target may also affect other material characteristics. The formulation should therefore be developed as a complete system rather than by optimizing a single microstructural variable.
The interfaces between WC grains and the metallic binder play a major role in cemented carbide behavior.
During liquid-phase sintering, the binder contributes to densification and forms a continuous or semi-continuous metallic phase within the WC structure.
The resulting microstructural interaction can influence:
The final interface condition is influenced by:
This is one reason why carbide microstructure cannot be understood from WC grain size alone.
The metallic binder should be distributed consistently throughout the intended microstructure.
Localized binder-rich or binder-lean regions can create variations in mechanical behavior and wear response. Depending on the material system:
Binder distribution is influenced by the complete manufacturing route, including:
Uniformity is therefore a manufacturing-control issue as well as a material-selection issue.
In cemented carbide, engineers may also consider the effective spacing and continuity of the metallic binder between WC grains. This relationship is sometimes described using concepts such as binder mean free path.
Binder mean free path is influenced by both:
Changes in this microstructural relationship can affect:
This demonstrates why grain characteristics and binder content should always be considered together. The same nominal binder percentage can produce different mechanical behavior when the WC structure and binder distribution are different.
WC grains are not necessarily identical in shape. Grain morphology can vary according to:
Morphology may influence:
However, grain shape should not normally be treated as an isolated purchasing criterion.
For most OEM applications, it is more useful to focus on verified material performance and controlled microstructure than to prescribe a specific grain morphology without a demonstrated functional requirement.
Abrasive wear can involve:
Where hardness-sensitive abrasion dominates, finer WC structures may provide an advantage.
However, abrasive-wear performance also depends on:
Abrasion does not automatically mean selecting the finest available WC grain size.
The material must still provide sufficient toughness and structural reliability for the actual loading conditions.
Particle erosion involves repeated impact of entrained particles against a component surface.
The material response may involve combinations of:
Erosion resistance often requires a balance between:
The appropriate WC structure therefore depends on factors such as:
There is no universal “erosion grain size.”
Where impact or severe mechanical loading is important, fracture resistance becomes a greater part of material selection.
A carbide selected only for maximum hardness may be less suitable if the component is exposed to:
In these situations, engineers may consider a microstructure that provides a more suitable balance of toughness and hardness.
However, material changes alone cannot compensate for poor component design. Impact-related performance also depends strongly on:
Grade selection and component design must therefore be reviewed together.
Temperature can influence carbide performance, but there is no single universal temperature at which all fine-grained or coarse-grained carbides become unsuitable.
Relevant factors include:
At elevated temperatures, wear behavior may change because several damage mechanisms can interact simultaneously.
For this reason, high-temperature carbide selection should not be reduced to a simple rule such as “use coarse grains above a specific temperature.” The complete thermal-mechanical environment must be evaluated.
In chemically aggressive environments, the metallic binder can become an important factor in material behavior.
Depending on the service medium, corrosion may preferentially affect the binder phase and reduce support around WC grains. This can contribute to combined mechanisms such as:
For certain applications, alternative binder systems, including nickel-based grades, may be considered when corrosion resistance is important.
However, binder selection must be based on the actual:
A corrosive environment does not automatically require a nickel-based binder.
A tougher carbide grade may be appropriate when failure analysis indicates that the existing microstructure is insufficiently tolerant of the actual mechanical loading.
This may occur in applications involving:
A tougher material balance may be developed through changes in:
However, increasing toughness may involve tradeoffs with:
A grade change should therefore be based on the identified failure mechanism rather than on the presence of fracture alone.
If a carbide component fractures, the material is not automatically the root cause.
The actual problem may involve:
In such cases, moving to a tougher microstructure may provide only limited improvement while leaving the underlying design problem unchanged.
A proper investigation should consider material, geometry, support, assembly, and operating load together.
For critical applications, carbide microstructure can be evaluated using appropriate metallographic and analytical methods.
Depending on the objective, these may include:
Powder-characterization methods should not be confused with measurements of the final sintered microstructure.
For example, the measured particle-size distribution of a starting powder does not directly define the WC grain-size distribution present in the material after milling, pressing, and sintering.
For most OEM components, it is generally more useful to specify the required material performance and an approved or verified carbide grade than to prescribe multiple microstructural manufacturing parameters without a clear engineering reason.
Depending on application criticality, a specification may include:
Detailed microstructural requirements may be justified for highly controlled, safety-critical, or previously validated applications.
However, specifications such as:
should generally be used only when supported by engineering validation, an applicable standard, or an established material specification.
Otherwise, overly prescriptive microstructural requirements can unnecessarily restrict manufacturing without guaranteeing better component performance.
Determine whether the component is primarily exposed to:
Evaluate:
Consider:
Consider:
Determine the relative importance of:
Use the required property balance to evaluate:
For critical applications, confirm the selected grade through:
There is no universal optimum WC grain size. The most suitable microstructure is the one that matches the application’s wear mechanisms, mechanical loading, environment, and component design.
In general:
The correct question is therefore not:
“What is the best WC grain size?”
It is:
“What microstructural balance is required for this component under its actual wear, loading, environmental, and design conditions?”
The microstructure of cemented tungsten carbide is an engineered material system rather than a single material parameter.
WC grain characteristics influence hardness, toughness, wear behavior, and fracture response, but they operate together with:
Finer structures may provide advantages under hardness-sensitive abrasive conditions. Microstructures designed for greater toughness may be more suitable when impact, bending, or other mechanical loads become important. Particle erosion, corrosion–wear interaction, and thermal-mechanical environments often require a more balanced material approach.
For this reason, carbide microstructure should not be selected from a universal grain-size chart.
The most reliable approach is to identify the dominant failure mechanisms, define the required property balance, select the grade and microstructure accordingly, and validate them under representative service conditions.
The best carbide grade is not necessarily the finest-grained, hardest, or toughest. It is the grade whose WC grain characteristics, binder system, microstructure, manufacturing quality, and component design are matched to the actual engineering application.
The metallic binder is not simply the “cement” holding WC grains together. It is an integral part of the microstructure that influences toughness, crack behavior, sintering, corrosion response, and overall material performance.
Cemented tungsten carbide is a composite material.
Its exceptional wear performance comes primarily from hard tungsten carbide (WC) grains, but the behavior of the finished material cannot be understood from the WC phase alone.
The metallic binder surrounding and connecting the WC grains plays an important role in:
Cobalt is the most widely established binder system in cemented tungsten carbide, but nickel-based and other engineered binder systems may be appropriate for specific applications.
The correct binder system is therefore not simply a choice between cobalt and nickel. It must be evaluated together with:
This article explains how metallic binder systems influence cemented tungsten carbide—and why binder selection should be treated as part of complete microstructural engineering.
The metallic binder performs several interconnected functions within cemented tungsten carbide.
The binder helps connect the WC grains into a dense composite structure.
During liquid-phase sintering, the binder participates in:
The effectiveness of this process depends on the complete formulation and processing conditions rather than on binder chemistry alone.
WC is extremely hard but has limited ability to accommodate deformation. The metallic binder provides a more ductile phase within the composite.
Depending on the complete microstructure, the binder can contribute to:
These mechanisms are influenced not only by binder content but also by:
The binder participates in transferring load between WC grains. This helps the composite function as an integrated material rather than as a collection of isolated hard particles.
However, load-bearing behavior depends on the complete microstructure, component geometry, support conditions, and applied stress state. The binder should therefore not be viewed as independently distributing all mechanical stresses.
Binder chemistry affects the thermodynamic and kinetic conditions during carbide manufacturing. It can influence:
Binder selection is therefore also a manufacturing and metallurgical consideration.
In some environments, the metallic binder can be more chemically active than the WC phase. Chemical attack on the binder may weaken support around WC grains and contribute to progressive material loss.
However, corrosion behavior is a property of the complete material–environment system. It depends on factors such as:
Corrosion resistance should therefore not be reduced to binder chemistry alone.
Binder content is an important variable in cemented carbide design.
In general, changing the relative amount of metallic binder changes the balance between:
A lower binder fraction generally increases the relative proportion of the hard WC phase. This can support higher hardness and strong resistance to certain forms of abrasive wear.
A higher binder fraction generally increases the amount of ductile metallic phase available to participate in deformation and crack-related mechanisms. Under appropriate microstructural and loading conditions, this can support greater toughness.
However, these trends should not be interpreted as universal rules. Final material behavior also depends on:
There is therefore no universally optimal binder percentage.
Binder content cannot be evaluated independently of the WC microstructure.
For a given nominal binder content, changes in WC grain characteristics can alter:
Likewise, two grades with a similar average WC grain size may behave differently if their binder content or binder distribution differs.
Binder content and WC grain characteristics are coupled microstructural variables. Neither should be selected in isolation.
One useful microstructural concept is the effective distance through the binder phase between WC grains, often described as binder mean free path.
This parameter is influenced by:
Changes in binder spacing can influence:
However, binder mean free path should not be treated as a single predictor of carbide performance. It is one part of the complete microstructural system.
Cobalt is the most widely established binder for cemented tungsten carbide.
Its broad use reflects several advantageous characteristics in properly designed WC–Co materials, including:
WC–Co grades can therefore be engineered for many industrial applications, including:
However, there is no single “WC–Co performance level.” Different WC–Co grades can vary substantially in:
Cobalt-based binders are widely useful, but they are not ideal for every environment.
Potential limitations may include:
The significance of these limitations depends strongly on the actual service environment. A cobalt-based carbide that performs well in one fluid or temperature range may behave differently in another.
The presence of an acidic, saline, oxidizing, or elevated-temperature environment should therefore trigger application-specific material evaluation—not automatic rejection of cobalt.
Nickel-based binders are used in some cemented carbide grades where a different balance of chemical and mechanical behavior is required.
Depending on the formulation and operating environment, nickel-based systems may provide advantages under certain chemically aggressive conditions.
Potential reasons for considering a nickel-based binder include:
Nickel is not universally more corrosion-resistant than cobalt under every condition.
Corrosion performance depends on:
A nickel-based grade should therefore be selected according to the actual environment rather than a general “corrosion-resistant” label.
Changing from cobalt to nickel affects more than corrosion behavior. It can also change:
WC–Ni should therefore not be treated as a direct one-for-one substitute for WC–Co at the same nominal binder percentage.
A properly engineered nickel-based grade may perform very well, but its properties must be evaluated as those of a distinct material system.
Nickel-based binders may be alloyed with other elements to adjust:
Chromium-containing nickel binder systems are one example. Other alloying approaches may also be used depending on the manufacturer, grade design, and intended application.
The specific chemistry should not be prescribed from a generic rule unless it has been validated for the service environment.
For OEM material selection, the more useful question is:
What binder chemistry and carbide grade have been validated for this combination of wear, chemistry, temperature, and mechanical loading?
Some cemented carbide materials use mixed or alloyed binder systems rather than predominantly cobalt- or nickel-based systems.
These may be developed to balance properties such as:
Iron-containing and other specialized binder systems also exist. Their suitability depends on the complete grade design.
They should not automatically be classified as inferior, superior, or low-cost materials solely on the basis of the primary binder element.
Some specialized carbide materials contain very little conventional metallic binder, while others are designed without a conventional cobalt- or nickel-rich binder phase.
Depending on their composition and manufacturing route, these materials may provide:
However, reducing or eliminating the conventional metallic binder also changes:
Such materials are specialized solutions rather than universally superior carbide grades.
In certain chemical environments, the metallic binder may be attacked more rapidly than the WC phase. This is often described as preferential binder attack.
As the binder degrades, the local WC structure can lose support. The sequence may involve:
This is particularly important when corrosion interacts with:
Cemented tungsten carbide is a multiphase material. Electrochemical interactions can therefore develop between the metallic binder and the WC-containing structure when the material is exposed to an electrolyte.
The resulting behavior depends on:
Under some conditions, the binder may preferentially dissolve. Under other conditions, different reactions or surface films may influence the corrosion process.
Electrochemical behavior should therefore be evaluated for the actual service medium.
Acidic or chemically aggressive fluids can increase the risk of binder degradation in some cemented carbide systems.
However, a general description such as “acidic service” is not sufficient for binder selection. Actual performance can depend on:
Different cobalt- and nickel-based formulations may behave differently under these conditions. Testing or validated service history is especially valuable for critical chemical-service applications.
At elevated temperatures, cemented carbide behavior can change because both the WC phase and metallic binder may participate in oxidation or other temperature-dependent reactions.
The significance depends on:
There is no single universal temperature above which all cobalt-bonded carbides become unsuitable or nickel-based carbides automatically become preferable.
Elevated-temperature performance must be evaluated as a complete material and service-condition problem.
Erosion and corrosion can interact in ways that accelerate material degradation. For example:
Total material loss can therefore differ from what would be expected from erosion or corrosion considered independently.
This interaction is particularly relevant in:
There is no universal binder system for all erosion–corrosion applications.
The appropriate choice depends on the balance between:
A nickel-based or alloyed binder may be advantageous in some environments. A cobalt-based grade may remain appropriate in others.
The correct decision requires evaluation of the complete wear–corrosion system.
When abrasive wear dominates, high hardness is often important. This may lead to consideration of grades with:
However, the lowest possible binder content is not automatically the best solution.
If the component also experiences:
additional toughness may be required. Binder content should therefore be matched to the complete loading and wear conditions.
Where impact or mechanical shock is important, a tougher grade may be required. This may involve adjusting:
However, simply increasing binder content does not guarantee adequate impact resistance.
Component performance also depends strongly on:
The binder system and component design must therefore be considered together.
Where corrosion and mechanical wear occur simultaneously, the binder must be evaluated against the actual chemical environment while the complete carbide grade must still provide adequate mechanical and wear performance.
Relevant factors include:
This is a more reliable approach than selecting nickel automatically whenever corrosion is present.
Coatings or other surface treatments may be useful in some applications, but they should not be treated as a universal solution to binder attack.
Their performance depends on:
If a coating is removed or damaged by abrasion, erosion, impact, or cracking, the behavior of the underlying carbide in the service environment again becomes important.
Surface treatment should therefore complement—not replace—appropriate base-material selection.
Selecting the correct binder chemistry and content is only part of the challenge. The binder must also be distributed consistently within the microstructure.
Manufacturing variables that can influence binder distribution include:
Poor local distribution can create regions with different:
For severe-service applications, manufacturing consistency is therefore as important as nominal binder composition.
Carbon balance is an important part of cemented carbide metallurgy.
The relationship between:
affects the phases that develop during sintering.
An unsuitable carbon balance can contribute to unwanted phases or other changes in microstructure. The acceptable processing window depends on the specific grade formulation.
Carbon control is therefore primarily a manufacturing and material-engineering responsibility rather than a simple OEM drawing parameter.
For most OEM components, the drawing does not need to prescribe the complete binder formulation.
More useful requirements may include:
Where the chemical environment is critical, the specification may also define:
A specific binder chemistry should be prescribed when there is a validated technical reason to do so.
Otherwise, allowing the carbide manufacturer to select and validate the complete grade can provide greater flexibility in meeting the required performance.
Determine whether performance is limited primarily by:
Identify:
Evaluate:
Consider:
Determine the required balance of:
Review:
For demanding applications, validation may include:
The binder is not simply a metallic “glue.” It is a structural, metallurgical, and chemical part of the cemented tungsten carbide composite.
Its effect cannot be separated from:
In general:
The correct question is not simply:
“Should this carbide use cobalt or nickel?”
It is:
“What binder–WC microstructure provides the required mechanical, wear, chemical, and manufacturing performance for this specific component?”
The metallic binder is one of the defining elements of cemented tungsten carbide.
It contributes to:
Cobalt is the most established binder platform for many industrial carbide grades, while nickel-based and other engineered binder systems can provide useful alternatives where a different balance of mechanical and environmental performance is required.
However, binder chemistry alone does not define carbide performance. Final behavior depends on the interaction between binder chemistry, binder content, WC grain characteristics, microstructural uniformity, manufacturing quality, component design, and service conditions.
Binder selection should therefore not be based on simple rules such as:
These trends may provide useful starting points, but the final material decision must reflect the complete engineering environment.
The best binder system is not necessarily cobalt, nickel, or the binder with the highest corrosion resistance or toughness when considered in isolation.
It is the binder system that enables the complete cemented carbide microstructure to deliver the required combination of wear resistance, mechanical reliability, environmental resistance, and manufacturing consistency in the actual application.
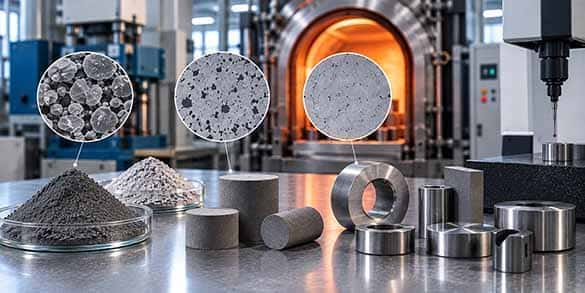
A cemented tungsten carbide component is not defined by composition alone. Powder preparation, milling, pressing, sintering, densification, finishing, and inspection all influence the microstructure that ultimately determines material consistency and service performance.
A cemented tungsten carbide component may be specified by grade, binder system, hardness, or other material properties, but those specifications describe only part of the finished material.
The required performance can be achieved consistently only when the manufacturing process produces the intended:
Manufacturing control therefore plays a central role in carbide performance.
Porosity, abnormal grain growth, local binder segregation, undesirable phases, cracks, contamination, or inconsistent densification can alter the behavior of an otherwise correctly selected carbide grade.
This article explains how powder preparation, formulation, milling, pressing, sintering, densification, finishing, and inspection influence the final microstructure of cemented tungsten carbide—and why density and porosity should be evaluated as part of a complete material-quality system rather than as isolated numbers.
Production of cemented tungsten carbide generally involves a sequence of controlled powder-metallurgy and finishing operations.
The exact route depends on:
Each stage can influence the next. Finished-carbide quality therefore cannot be separated from manufacturing consistency throughout the complete process chain.
The properties of cemented carbide begin with the raw materials.
Relevant powder characteristics may include:
WC powder characteristics influence the development of the final WC grain structure, but powder particle size should not be treated as identical to the WC grain size present after sintering.
Grain evolution occurs during milling and sintering, and the final microstructure depends on the complete formulation and thermal history.
Binder powders must also be controlled because their chemistry, particle characteristics, and distribution influence mixing, sintering, and the final WC–binder structure.
For most OEM applications, customers do not need to prescribe every raw-powder parameter. More useful requirements usually focus on:
Detailed raw-material specifications are more appropriate when they have been validated for a critical application.
Formulation determines the intended material composition before consolidation and sintering. It can include control of:
Formulation must be repeatable because relatively small variations can change the resulting microstructure and material properties.
End-product performance therefore depends not only on using the correct nominal ingredients but also on controlling their proportions consistently.
Binder content influences the balance between hardness, toughness, fracture behavior, and wear performance.
In general:
However, binder content does not determine performance by itself. Its effect depends on:
Manufacturing control must therefore reproduce the complete grade—not simply a target binder percentage.
Carbon balance is an important metallurgical variable in cemented tungsten carbide.
Depending on the composition and processing conditions, an unsuitable carbon condition can promote the formation of undesirable phases or free carbon. These changes can affect:
The appropriate carbon-processing window depends on the specific carbide formulation. Carbon control is therefore primarily a manufacturing and material-engineering responsibility rather than a value that should automatically be prescribed on every OEM drawing.
Some carbide grades use additions intended to influence WC grain growth during sintering.
Depending on the grade design, these may include chromium-, vanadium-, tantalum-, or other carbide-forming additions. Their purpose may include:
Such additions are grade-specific. More is not necessarily better, and no particular addition should be treated as universally required for high-performance carbide.
Milling is more than particle-size reduction. It is a critical stage for creating a uniform mixture of WC powder, binder powder, additives, and processing constituents.
Relevant variables can include:
The process must promote consistent distribution without introducing unacceptable contamination or uncontrolled changes to the powder system.
Poor mixing can result in local variations in binder distribution, grain development, hardness, density, or mechanical behavior.
After milling, the powder mixture may be conditioned into a form suitable for pressing. Depending on the manufacturing route, this can involve granulation or spray drying.
Important characteristics may include:
The objective is to provide predictable die filling and stable compact formation. Inconsistent granulation can contribute to variations in green density, shrinkage, and dimensional consistency.
Before sintering, the carbide powder must be formed into a compact with sufficient strength and an appropriate density distribution.
Possible forming methods include:
No single pressing method is universally superior. The appropriate method depends on geometry, component size, production quantity, material grade, dimensional requirements, and process capability.
A pressed compact does not yet have its final dimensions. Substantial shrinkage occurs during sintering.
If green density is inconsistent, different regions of the part may shrink differently. This can contribute to:
Green-density control becomes increasingly important as components become larger, thicker, geometrically complex, or sensitive to final tolerances.
Sintering transforms the formed powder body into a dense cemented carbide microstructure.
During the sintering cycle, several processes can occur, including:
The required temperature–time cycle depends on the grade and manufacturing process. There is no universal sintering temperature that represents the optimum condition for all cemented carbides.
Forming agents and other temporary processing constituents must be removed appropriately before or during the early stages of the thermal cycle.
Poor control may contribute to:
Debinding conditions depend on the processing aid, component geometry, heating rate, atmosphere, and furnace cycle.
In conventional cemented carbide systems, the metallic binder participates in liquid-phase sintering. This enables:
Successful densification depends on more than temperature alone. Important variables include:
Sintering should therefore be understood as a controlled metallurgical process rather than simply heating the pressed part until it becomes dense.
Time and temperature influence both densification and WC grain evolution.
Insufficient thermal conditions may leave excessive residual porosity, incomplete microstructural development, or unsuitable phase conditions.
Excessive thermal exposure may contribute to:
The objective is not to use the highest possible temperature or longest holding time. It is to achieve the intended density, phase balance, and microstructure reproducibly.
Cooling is also part of the sintering process. Cooling conditions can influence:
The significance varies with grade, component geometry, furnace process, and atmosphere. Controlled cooling is therefore another element of manufacturing consistency.
Density is an important inspection parameter for cemented carbide. It can help indicate whether the finished material is consistent with the expected composition, binder content, porosity level, and degree of densification.
However, density is not a complete measure of carbide quality.
Two components can have similar measured density while differing in:
Density should therefore be interpreted together with other inspection results.
Porosity refers to voids remaining in the sintered microstructure.
Depending on pore size, amount, distribution, location, component geometry, and service loading, porosity may influence:
Porosity in a highly stressed or functionally critical region may be more significant than the same amount located elsewhere. Porosity assessment should therefore consider not only how much porosity is present but also its type and distribution.
A component with low measured porosity can still have other material-quality concerns, including:
Low porosity is an important quality indicator, but it is not equivalent to complete material quality.
Some carbide manufacturing routes use pressure-assisted densification, including integrated sinter-HIP or other hot isostatic pressing processes.
When appropriately applied, these processes can help reduce certain residual pores and improve densification. Potential benefits may include:
However, HIP is not automatically required for every high-quality carbide component. Its value depends on grade design, initial sintering quality, component requirements, pore characteristics, service loading, and manufacturing capability.
Properly controlled conventional sintering and sinter-HIP can both produce suitable materials when correctly matched to the grade and application.
Pressure-assisted densification should not be treated as a universal repair process. It may not correct problems such as:
The first objective must remain to prevent defects through correct powder preparation, formulation, pressing, and sintering.
HIP, where used, is part of the manufacturing strategy—not a substitute for process control.
After sintering, many cemented carbide components require precision finishing. Depending on the design, this may include:
These operations establish final dimensions, tolerances, surface finish, sealing or mating surfaces, and other functional geometry.
However, finishing processes can affect surface integrity if they are not controlled correctly. Possible concerns include:
Finishing is therefore part of material performance—not simply a cosmetic or dimensional operation.
Not every surface requires the same finish. The required surface condition depends on its function, which may involve:
Specifying unnecessarily tight surface-finish requirements can increase manufacturing complexity without improving component performance.
OEM drawings should therefore distinguish critical functional surfaces from non-critical surfaces.
Possible contributing factors include powder or granule condition, inconsistent pressing, incomplete densification, unsuitable thermal conditions, contamination, or trapped gases.
Possible effects include local stress concentration, reduced mechanical reliability, and increased susceptibility to material removal.
Possible contributing factors include formulation, grain-growth control, carbon balance, thermal history, and powder characteristics.
Possible effects include local changes in hardness, altered fracture behavior, and non-uniform wear response.
Possible contributing factors include incomplete mixing, powder segregation, binder migration, or inconsistent processing.
Possible effects include local differences in hardness and toughness, changes in corrosion behavior, and inconsistent mechanical response.
Cracks may arise during pressing, handling, debinding, sintering, cooling, grinding, EDM, assembly, or subsequent service.
Their significance depends on their location, orientation, size, and the applied loading.
Changes in carbon balance, contamination, formulation, or atmosphere control can produce microstructural conditions different from the intended grade.
These conditions may affect material properties even when the component appears dimensionally acceptable.
Final inspection should verify that manufacturing has produced the intended component and material condition.
Depending on application requirements, inspection may include:
Not every component requires every inspection method. The inspection plan should be matched to application criticality, component geometry, failure consequences, material specification, and manufacturing history.
Density measurement can be a useful production-control tool.
A value that differs from the expected range for the grade may indicate possible variation in composition, binder content, porosity, or process condition.
However, density alone cannot identify the underlying cause. It should be considered together with hardness, metallography, composition, or other appropriate controls when investigating unexpected results.
Hardness testing is widely used to verify the consistency of cemented carbide. It may help identify deviations related to:
However, hardness is not by itself a direct measurement of binder content or sintering quality.
Two materials can have similar hardness while differing in toughness, porosity, microstructure, or corrosion behavior. Hardness should therefore be interpreted as one part of the complete material-verification process.
Metallographic or microscopic examination can provide information about:
This is particularly valuable when validating a new grade, investigating a failure, qualifying a manufacturing process, or controlling critical severe-service components.
Depending on component geometry and defect type, non-destructive inspection methods may sometimes be used to identify internal or surface discontinuities.
The suitability and sensitivity of a particular method depend on:
Non-destructive testing should therefore be selected and validated for the specific inspection objective rather than applied automatically.
For most OEM carbide components, the customer does not need to specify every manufacturing parameter.
Useful requirements may include:
The following manufacturing details normally remain under manufacturer control unless there is a validated technical reason to specify them:
This approach focuses the OEM specification on required performance and verifiable material condition while allowing the manufacturer to control the process used to achieve them.
Confirm that WC and binder materials are controlled, formulation is repeatable, contamination is controlled, and batch traceability is appropriate.
Assess whether the manufacturing route provides consistent composition, binder distribution, additive distribution, and powder condition.
Evaluate whether pressing or forming provides stable green geometry, suitable density distribution, and repeatable shrinkage behavior.
Confirm control over:
Evaluate, as appropriate:
Confirm dimensions, surface finish, edge condition, grinding quality, EDM condition where applicable, and other functional features.
For critical applications, correlate manufacturing and inspection results with laboratory testing, prototype evaluation, field performance, failure analysis, or established service history.
A carbide grade defines an intended material system. Manufacturing control determines whether that material system is reproduced consistently in the finished component.
Density, porosity, and microstructural uniformity are important indicators, but none should be considered independently.
Reliable performance depends on the interaction of:
The correct question is therefore not simply:
“Is the carbide dense enough?”
The correct question is:
“Has the manufacturing process produced the intended carbide grade with the required density, microstructure, surface integrity, dimensional quality, and consistency for this application?”
Cemented tungsten carbide performance is created through a complete manufacturing sequence.
Powder preparation, formulation, milling, forming, sintering, densification, finishing, and inspection all influence the final microstructure.
Good manufacturing control aims to achieve:
Porosity and density are important quality indicators, but they do not provide a complete definition of carbide quality.
A component can have high density and still contain microstructural or surface conditions that affect performance. Conversely, the significance of a small microstructural feature depends on its type, location, component geometry, and service loading.
The most reliable approach is therefore to evaluate material composition, microstructure, manufacturing consistency, inspection results, and actual service requirements together.
The same nominal carbide grade can perform differently when manufacturing quality differs. For severe-service OEM components, consistent control of the entire process is therefore as important as selecting the correct grade in the first place.
The chemistry defines the material system.
The manufacturing process develops the microstructure.
The microstructure, together with component design and service conditions, determines performance.
Maximum hardness is not always desirable. The most suitable cemented tungsten carbide grade is the one that provides the required balance of hardness, toughness, wear resistance, and fracture reliability for the component’s actual wear mechanisms, loading conditions, geometry, environment, and service requirements.
One of the most common assumptions in tungsten carbide selection is that a harder grade must automatically be a better grade.
That assumption is understandable.
Cemented tungsten carbide is often selected because of its exceptional hardness and wear resistance, so it may seem logical to specify the highest hardness available.
In practice, however, maximum hardness is not always the correct engineering objective.
A carbide component may need to resist:
Increasing resistance to one failure mechanism can change the material’s response to another.
For this reason, hardness and toughness should not be treated as independent properties that can simply be maximized simultaneously.
The engineering objective is to achieve the appropriate property balance for the actual application.
This article explains why hardness and toughness are linked to cemented carbide microstructure, how different loading and wear conditions change the required balance, and why geometry, support, assembly, and service conditions must be considered together with carbide grade.
Hardness and toughness describe different aspects of material behavior.
Hardness describes resistance to localized deformation, indentation, scratching, and related forms of surface damage.
In severe-service carbide applications, higher hardness may help resist mechanisms such as:
However, hardness alone does not describe how the material behaves when cracks initiate or when the component experiences impact, bending, or complex stress.
Toughness broadly describes a material’s ability to absorb energy, tolerate damage, and resist fracture under mechanical loading. Fracture toughness is a specific measured property used to characterize resistance to crack propagation.
In cemented tungsten carbide, toughness is relevant to conditions involving:
A tougher carbide is not necessarily “soft.”
It remains a very hard composite material, but its microstructure provides a different balance between resistance to surface material removal and resistance to fracture.
Cemented tungsten carbide consists primarily of:
The WC phase provides much of the material’s hardness and resistance to abrasive material removal.
The binder contributes to:
Changing the relative amount and arrangement of these phases changes the behavior of the composite.
In general:
However, this relationship is not controlled by one variable alone.
It also depends on:
The hardness–toughness relationship should therefore be understood as a microstructural balance, not as a simple formula.
WC grain characteristics influence both hardness and fracture behavior.
Finer WC structures generally tend to support higher hardness under otherwise comparable conditions.
This can be beneficial where resistance to:
is particularly important.
Coarser or otherwise tougher microstructural designs may provide greater tolerance to certain crack-related loading conditions.
However:
Fine WC does not automatically mean “brittle,” and coarse WC does not automatically mean “tough.”
Actual behavior depends on the complete grade, including:
WC grain size should therefore never be selected independently from the rest of the microstructure.
Binder content also influences the hardness–toughness balance.
In general, a lower relative binder fraction increases the proportion of the hard WC phase and can support higher hardness.
A higher binder fraction can provide more metallic phase to participate in deformation and crack-related mechanisms.
But the relationship is not linear or universal.
The effect of binder content depends on:
For this reason, rules such as:
should be treated only as broad starting trends.
They are not complete grade-selection rules.
The effective spacing of the metallic binder between WC grains is another factor affecting mechanical behavior.
Changes in binder mean free path can influence:
However, binder mean free path is not an independent performance metric.
It must be considered together with:
Crack propagation in cemented tungsten carbide is more complex than a simple choice between “through the WC grain” or “through the binder.”
Depending on the grade and loading condition, cracks may propagate:
The crack path can be influenced by:
Depending on its design, a tougher microstructure may increase resistance to crack propagation through mechanisms such as:
But no single crack mechanism explains the behavior of all carbide grades.
A carbide grade cannot be fully evaluated using hardness and toughness alone.
Other relevant properties may include:
Different applications place different importance on these properties.
For example, a component operating primarily under compressive loading may have different requirements from a thin carbide section exposed to bending or edge impact.
Therefore, hardness and toughness should be treated as two important parts of a larger property system.
In abrasion-dominated service, resistance to surface material removal is often a primary requirement.
Typical mechanisms may include:
Higher hardness can be beneficial under these conditions.
However, abrasion severity also depends on:
Therefore:
Abrasion does not automatically mean selecting the hardest available carbide grade.
If the component also experiences impact, vibration, edge loading, bending, or assembly stress, an excessively hardness-focused grade may not provide the best overall reliability.
The correct objective is sufficient hardness without sacrificing the mechanical reliability required by the application.
Particle erosion differs from simple sliding abrasion.
High-velocity particles may produce combinations of:
The optimal hardness–toughness balance therefore depends on:
A very hard grade may perform well in some erosive conditions.
In others, localized impact or microfracture may make additional toughness important.
There is no universal hardness value or carbide grade for erosion.
Impact introduces a different type of risk.
Instead of gradual surface wear, failure may involve:
In these conditions, increasing fracture tolerance may be more important than maximizing hardness.
A tougher carbide grade may be considered when failure analysis shows that the existing material cannot adequately tolerate:
However, a tougher grade cannot compensate indefinitely for poor component design.
Impact performance must also be addressed through:
Many industrial applications do not experience a single dominant wear mechanism.
A component may undergo continuous abrasion with occasional impact.
Examples can include components exposed to:
In these applications, neither maximum hardness nor maximum toughness is necessarily appropriate.
The grade must provide enough hardness to control progressive wear while maintaining enough fracture resistance to survive mechanical events.
This is one reason why grade selection should be based on the complete operating condition rather than a single datasheet number.
Cemented tungsten carbide performs especially well under compressive loading, but it is more sensitive to tensile and bending stresses.
Under bending, one side of the component experiences tensile stress.
Existing flaws or stress concentrations can then become important crack-initiation sites.
Relevant factors include:
Flexural or transverse rupture strength can provide useful comparative information, but it should not be interpreted as a complete prediction of component bending performance.
Test values are influenced by:
Component design remains essential.
Temperature changes can create mechanical stresses even when external loading is limited.
Potential contributors include:
Under these conditions, toughness may become an important consideration.
However, “thermal cycling means choose a tougher grade” is too simple.
The complete evaluation should consider:
The solution may require material changes, design changes, or both.
Chemical environments can modify the hardness–toughness discussion.
If the binder phase is preferentially attacked, the local support of WC grains may weaken.
This can increase susceptibility to:
Therefore, a grade that provides a suitable mechanical balance in a dry environment may not perform the same way in:
Hardness and toughness must therefore be evaluated together with environmental resistance.
Even a correctly selected carbide grade can fail if the component geometry creates an unfavorable stress state.
Important stress concentrators may include:
These features can create highly localized stresses that initiate cracks.
Selecting a tougher carbide may increase tolerance, but redesigning the geometry may provide a more effective solution.
Carbide components often operate as part of a larger assembly.
The surrounding steel or other supporting material can strongly influence how the carbide is loaded.
Poor support can create:
Even a relatively tough carbide grade may fracture if a section is inadequately supported.
Therefore:
The grade determines the material’s resistance to the applied stress state, but geometry, support, and assembly help determine what that stress state actually is.
Both must be engineered together.
Press fits and shrink fits can introduce beneficial retention, but they can also generate significant stresses in carbide components.
Excessive interference, uneven contact, geometric errors, or poor surface condition can create:
If the root cause is excessive assembly stress, changing to a tougher grade may improve tolerance but may not solve the underlying problem.
The assembly design should be reviewed first.
A tougher carbide grade may be worth evaluating when failure analysis shows evidence of:
The grade adjustment may involve changes to:
However, the grade should be evaluated together with geometry and loading.
Changing to a tougher grade may not solve failures caused primarily by:
In these cases, the material may be responding to a design or service problem rather than representing the root cause.
A grade change can sometimes delay failure without eliminating it.
A harder grade may be worth evaluating when:
But the correct question is not simply:
“Can we use a harder grade?”
It is:
“Can additional hardness reduce the dominant wear mechanism without creating an unacceptable increase in fracture risk?”
Increasing hardness can be counterproductive when the component is already limited by:
In these cases, reduced tolerance to cracking may offset any improvement in abrasive wear resistance.
A harder grade should therefore not be used as an automatic response to short service life.
A worn or fractured carbide component can provide valuable information about the dominant failure mechanism.
Useful observations may include:
However, visual appearance alone may not always identify the complete root cause.
For critical failures, additional evaluation may include:
The objective is not simply to classify the component as “too hard” or “too soft.”
It is to determine why the component lost functionality.
A simple rule such as:
can be useful as an initial clue, but it is not a complete engineering diagnosis.
For example:
Failure analysis should therefore consider the complete system.
Hardness values are useful for characterizing and comparing carbide grades.
However, a higher hardness number does not mean the material is universally “better.”
Two grades with similar hardness may differ in:
Likewise, a modest difference in hardness may or may not produce a meaningful service-life difference.
Hardness should therefore be interpreted together with other material and application information.
Fracture-toughness or strength measurements can help compare carbide grades, but they are not complete service-performance predictions.
Measured values can depend on:
A grade with a higher laboratory toughness value may still fail in service if:
Material data should inform engineering decisions—not replace them.
A more reliable selection approach is:
Determine whether the component is primarily affected by:
Review:
Check for:
Consider:
Determine how much emphasis the application requires on:
Evaluate:
Validation may involve:
Maximum hardness is not automatically the objective. Maximum toughness is not automatically the objective either.
The engineering objective is to achieve the property balance required by the actual component and service condition.
In general:
But none of these statements is a universal grade-selection rule.
The better question is not:
“What is the hardest carbide grade?”
or:
“What is the toughest carbide grade?”
It is:
“What balance of hardness, toughness, wear resistance, fracture reliability, and environmental performance is required for this specific component under its actual operating conditions?”
The hardness–toughness relationship is one of the central design considerations in cemented tungsten carbide.
WC grain characteristics, binder system, binder content, microstructural quality, porosity, and manufacturing control all influence how the material balances resistance to wear with resistance to fracture.
Hardness is important because it helps resist material removal.
Toughness is important because it helps the material tolerate crack-related and mechanical loading.
But neither property should be maximized without considering the rest of the system.
A carbide component that wears gradually may require a different material balance from one that chips, cracks, bends, or experiences repeated impact.
And a component that fractures may not necessarily need a different grade at all—the root cause may be geometry, support, assembly, surface condition, or loading.
For this reason, carbide selection should combine:
wear mechanism + mechanical loading + geometry + support + environment + microstructure + manufacturing quality + validation.
The best carbide grade is not necessarily the hardest available or the toughest available.
It is the grade that provides the most appropriate balance of wear resistance and mechanical reliability for the actual application.
The material system defines the available properties. The microstructure establishes the hardness–toughness balance. The component design and service conditions determine which balance is required.

Learn how hardness, toughness, WC grain characteristics, binder system, geometry, and loading conditions interact to influence cemented tungsten carbide performance.

Learn how powder preparation, pressing, sintering, densification, porosity control, microstructural uniformity, finishing, and inspection influence the consistency and performance of cemented tungsten carbide.

Learn how cobalt, nickel, binder content, WC–binder interaction, and microstructural control influence toughness, wear resistance, corrosion response, sintering, and overall performance in cemented tungsten carbide.

Learn how WC grain characteristics, grain-size distribution, binder interaction, microstructural uniformity, and manufacturing control influence the hardness, toughness, wear resistance, and fracture behavior of cemented tungsten carbide.